The global commercial food manufacturing ecosystem is undergoing a structural transition toward clean-label, low-moisture plant ingredients. As a leading China dehydrated vegetable powder manufacturer and international procurement distributor, our technical infrastructure bridges agricultural origins with strict high-speed food processing specifications. Dehydrated vegetable powders—spanning Air-Dried (AD) garlic, onion, tomato, spinach, and high-purity functional extracts—serve as essential structural matrices, flavor enhancers, natural colorants, and micronutrient carriers across modern food processing sectors.
Industrial food formulators face increasing complexity when securing raw materials: managing volatile bulk moisture levels, preventing clumping without micro-encapsulation additives, maintaining heat-sensitive volatile aromatic compounds, and assuring stringent microbiological safety parameters (including zero Salmonella, E. coli, and low Total Plate Counts). By integrating advanced continuous dehydrators, automated micro-milling systems, and high-efficiency HTST (High-Temperature Short-Time) sterilization technology, China's ingredient manufacturing sector provides global buyers with enterprise-grade consistency, scalable volume, and reduced landed costs.
Information Gain Insight: Modern automated dehydrators utilize multi-stage temperature zone management (60°C to 85°C) coupled with humidity-controlled exhaust vectors. This prevents surface case-hardening while achieving equilibrium moisture content (EMC) under 5.0%, preserving natural enzymatic profiles and aromatic terpenes.
Selecting the appropriate dehydration thermal vector depends directly on end-use application parameters, structural reconstitutability requirements, and cost-to-performance ratios. Our processing facilities operate three distinct dehydration lines:
| Processing Parameter | Air-Dried (AD) Powders | Freeze-Dried (FD) Powders | Spray-Dried (SD) Extracts |
|---|---|---|---|
| Moisture Content (% w/w) | ≤ 5.0% - 6.5% | ≤ 2.0% - 3.5% | ≤ 4.0% - 5.0% |
| Water Activity (aw) | 0.25 - 0.35 | 0.15 - 0.25 | 0.20 - 0.30 |
| Mesh Granularity Range | 40 Mesh to 120 Mesh | 60 Mesh to 200 Mesh | 80 Mesh to 250 Mesh |
| Rehydration Index | Moderate (1:4 in warm water) | Instant (1:8 in cold/warm water) | Complete Solubility |
| Nutritional Retention | 80% - 88% (Heat stable) | 95% - 98% (Heat sensitive) | 85% - 92% (Standardized) |
| Primary B2B Applications | Soups, Sauces, Meat Rubs, Instant Noodles | Nutraceuticals, Infant Food, Premium Bakery | Beverage Bases, Functional Supplements |
Strategic sourcing directors and research & development managers must anticipate consumer-driven shifts and supply chain regulatory pressures. Based on market intelligence and cross-border distribution analytics, four macro-trends are reshaping global procurement for dehydrated vegetable powders and functional ingredients:
Global consumer demand for clean labels has driven industrial food processors to phase out synthetic silicon dioxide (E551) and sodium aluminosilicate. Formulators now demand dehydrated powders milled under strict ambient humidity conditions (<35% RH) that achieve high bulk density and natural free-flowing characteristics without chemical flow additives.
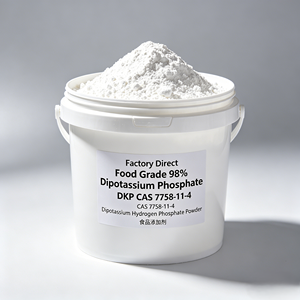
Enterprise procurement teams are migrating away from fragmented multi-vendor sourcing models. Consolidating specialized hydrocolloids, vegetable powders, emulsifiers (GMS/DMG), and food-grade phosphates (MSP/DKP) under a single consolidated purchase order slashes customs freight handling fees, lowers working capital lockup, and ensures unified quality documentation.
Standard vegetable nutrition is being upgraded through enzymatic hydrolysis. Products like 98% Peanut Oligopeptide Powder and high-purity Spirulina extracts reflect the convergence of savory food manufacturing with nutraceutical efficacy, demanding precise molecular weight control (<1000 Daltons) for rapid human metabolic absorption.
Corporate sustainability mandates are shifting sourcing benchmarks toward low-carbon dehydration facilities. Utilizing solar-assisted thermal exchangers, closed-loop water recovery systems, and direct farm-contracted crops allows global food brands to report fully verifiable Scope 3 carbon reduction metrics.
Raw material integrity dictates final product performance. Our contract farming network spans pesticide-monitored agricultural zones across East Asia. Every batch of raw garlic, spinach, carrot, and tomato undergoes rigorous screening for heavy metals (Pb, Cd, As, Hg), organochlorine pesticide residues, and mycotoxins prior to entering the washing, slicing, and drying tunnels.
Through digital lot-tracking systems, each 20kg carton or 25kg vacuum-sealed bag shipped to international co-packers can be traced directly back to its agricultural origin, harvest date, thermal processing log, and analytical Certificate of Analysis (CoA).
As a trusted sourcing partner and direct manufacturer, our infrastructure is tailored to eliminate operational friction for food R&D formulators, plant procurement specialists, and brand managers. We combine deep raw material stock holdings with custom processing flexibility:
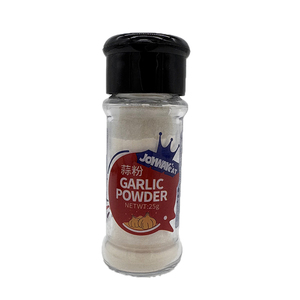
From staple AD Dehydrated Garlic Powder and Natural Yeast Extract to specialized food phosphates (MSP, DKP) and emulsifiers (GMS DMG), our catalog covers comprehensive functional food manufacturing requirements under one roof.
Engineered particle sizing from coarse 40-mesh granules for meat rubs down to ultrafine 200-mesh micro-powders for instant beverage premixes. Custom dry-blending capability ensures homogenous dispersion of multi-component seasonings.
Our processing plants maintain BRCGS, ISO 22000, HACCP, Kosher, and Halal certifications. Every product lot undergoes internal HPLC, ICP-MS, and microbiological testing prior to release, guaranteed by detailed CoAs.
Protect your working capital. Combine multiple product categories—such as savory powders, spirulina, yeast extracts, and bakery emulsifiers—into single container loads (FCL) or pallet-consolidated LCL shipments with minimal MOQs.
Our in-house food technologists provide hands-on technical guidance for matrix replacement, clean-label sodium reduction, fat emulsification, and moisture retention optimization in industrial bakery, savory, and pet food applications.
With strategic warehousing hubs in North America and Asia, backed by long-standing freight partnerships, we ensure short lead times, reliable customs compliance, and on-time, in-full delivery to your plant's loading dock.
Dehydrated vegetable powders and associated functional ingredients perform vital physical and sensory roles across diverse food matrices. Below is an overview of how our raw material portfolio elevates product formulations:
In high-speed commercial baking, achieving uniform crumb structure, dough elasticity, and anti-staling shelf stability is paramount. Food Grade GMS DMG Glycerol Monostearate acts as a potent starch-complexing emulsifier, reducing amylose retrogradation. When paired with Monosodium Phosphate (MSP) for controlled leavening kinetics, bakery lines maintain consistent volume, softness, and moisture distribution across extended retail shelf lives.
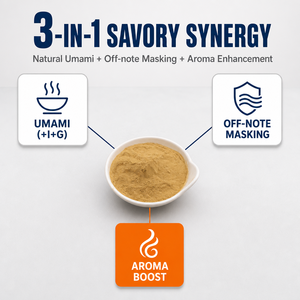
Spicy AD Dehydrated Garlic Powder and high-purity Natural Yeast Extract Powder form the flavor backbones for snack seasonings, ramen broths, marinades, and ready-to-eat meals. Natural yeast extract provides rich Umami impact (via natural free glutamates and 5'-ribonucleotides) allowing food formulators to reduce overall MSG and sodium content while boosting mouthfeel and flavor depth.
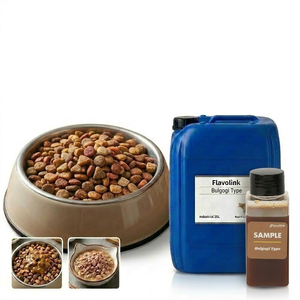
Pet food palatability requires specialized flavor enhancement and nutrient-dense carriers. Products such as Flavolink Pet Food Enhancer Liquid and high-protein Spirulina Powder provide essential amino acids, anti-inflammatory carotenoids, and enticing aroma profiles tailored for extruded kibble coatings, wet pet food gravies, and functional animal treats.
Modern beverage formulations leverage bio-available protein fractions. 98% Peanut Oligopeptide Powder offers complete cold-water solubility, low viscosity, and heat stability under UHT pasteurization. Derived via targeted enzymatic cleavage, these low-molecular-weight peptides deliver rapid nutritional recovery for active nutrition beverages, health shakes, and dietary supplements.
Get clear answers regarding technical specifications, minimum order quantities, compliance documentation, and international shipping logistics:
We utilize High-Temperature Short-Time (HTST) steam sterilization and controlled hot-air thermal processing to eliminate pathogens such as Salmonella, E. coli, and Listeria monocytogenes without scorching the powder or degrading essential volatile oil profiles. Every batch undergoes validated micro-testing to meet international food safety requirements (TPC < 100,000 CFU/g, Yeast & Mold < 500 CFU/g, Salmonella Negative / 25g).
Yes. We offer fully customizable particle sizing ranging from coarse granules (10–40 mesh) down to fine micro-powders (80–200 mesh). Packaging options include standard 25kg multi-wall kraft paper bags with inner polyethylene liners, 20kg moisture-barrier cartons, fiber drums, and 500kg–1000kg bulk super-sacks (FIBC) tailored to your factory's automated dumping station specifications.
Rather than managing multiple factory orders, minimum order quantities (MOQs), and separate freight bills, you can consolidate dehydrated vegetable powders, emulsifiers (GMS DMG), food phosphates (MSP/DKP), spirulina, and yeast extracts into a single purchase order. We assemble, palletize, quality-verify, and ship your consolidated order under one master Bill of Lading (BOL) and single entry customs invoice.
Every shipment is accompanied by a batch-specific Certificate of Analysis (CoA) verified by our certified QA laboratory. Standard documentation includes BRCGS/ISO 22000 certificates, Allergen Statements, Non-GMO Declarations, Heavy Metal Analysis (ICP-MS), Pesticide Residue Test Reports, Kosher, and Halal certifications. FDA Food Facility Registration details and US-FDA Prior Notice documents are provided for US-bound freight.
When stored in original unopened moisture-barrier packaging at cool ambient temperatures (< 20°C / 68°F) and relative humidity below 60%, our AD dehydrated vegetable powders maintain a certified shelf life of 24 months from the manufacturing date. We recommend storing products off concrete floors on wooden or plastic pallets away from direct light exposure.
For standard stocked items (such as AD Garlic Powder, Spirulina Powder, MSP, and DKP), our dispatch lead time is 7 to 10 working days from PO confirmation. For custom mesh milling or special OEM blends, lead times are typically 14 to 21 days. Standard export MOQs start at 1,000 kg (1 metric ton), with smaller sample pallet trial runs available upon technical evaluation.
Partner with China's premier dehydrated vegetable powder manufacturer and ingredient consolidation specialist. Contact our technical sales team for factory-direct quotes, technical specification sheets, and complimentary R&D sample kits.
Get a Quote