Explore our consolidated portfolio of high-purity sweeteners, structural food ingredients, flavor enhancers, and high-shear processing equipment tailored for food and beverage operations in Azerbaijan and Eurasia.
The food and beverage sector in Azerbaijan, anchored by major manufacturing hubs in Baku, Sumqayit, and Ganja, is undergoing a profound structural shift toward health-conscious, low-glycemic, and sugar-reduced product reformulations. Driven by non-communicable disease awareness campaigns led by the Food Safety Agency of the Republic of Azerbaijan (AQTA) and expanding consumer preference for keto-friendly and diabetic-safe foods, commercial food producers face an urgent imperative to replace traditional sucrose without compromising texture, mouthfeel, or processing stability.
Erythritol (CAS No. 149-32-6), a four-carbon sugar alcohol (polyol) produced via natural bio-fermentation of Non-GMO corn starch, has emerged as the premier functional sugar replacement for Azerbaijani food engineers. Exhibiting 70% of the relative sweetness of sucrose with virtually zero caloric contribution (less than 0.2 kcal/g), zero glycemic index (GI = 0), and an exceptionally high digestive tolerance, Erythritol provides the exact physical bulk, crystalline structure, and clean taste profile required by modern processing lines. As direct Chinese manufacturing operations supply over 80% of the global polyol market, establishing a direct, verified factory supply corridor from China to Azerbaijan represents the most cost-effective, scalable solution for enterprise purchasing teams.
Unlike high-intensity artificial sweeteners (such as aspartame or acesulfame-K) which lack structural body, Erythritol acts as a true bulk sweetener. Its unique chemical architecture yields distinct thermodynamic and rheological properties essential for industrial food formulations.
| Parameter / Specification | Standard Crystalline Grade | Micronized Powdered Grade | Coarse Granular Grade |
|---|---|---|---|
| Particle Mesh Size | 18 - 60 Mesh (250 - 1000 μm) | 100 Mesh (< 150 μm) | 12 - 30 Mesh (600 - 1500 μm) |
| Assay (Dry Basis) | 99.5% – 100.5% | 99.5% – 100.5% | 99.5% – 100.5% |
| Melting Point (°C) | 118°C – 123°C | 118°C – 123°C | 118°C – 123°C |
| Solubility in Water (25°C) | 37% (w/w) | Fast-Dissolving 37% (w/w) | 37% (w/w) Slow Release |
| Heat of Solution (Endothermic) | -43 cal/g (Strong Cooling Effect) | -43 cal/g (Immediate Release) | -43 cal/g (Controlled Cooling) |
| Loss on Drying | ≤ 0.20% | ≤ 0.30% | ≤ 0.15% |
| Residue on Ignition (Ash) | ≤ 0.10% | ≤ 0.10% | ≤ 0.10% |
| Heavy Metals (as Pb) | ≤ 5 ppm | ≤ 5 ppm | ≤ 5 ppm |
| Primary Target Application | Beverages, Tabletop Sweeteners | Chocolate, Bakery Icings, Confectionery | Sachet Packaging, Hard Candies |
Reformulating regional culinary favorites and modern FMCG goods requires precise functional knowledge of how Erythritol interacts with fats, proteins, hydrocolloids, and thermal processing cycles.
In Azerbaijan’s high-sugar pastry sector, replacing sucrose syrup with Erythritol requires managing its high crystallization tendency. R&D teams utilize a 70:30 blend of Erythritol and polydextrose or soluble corn fiber to prevent post-bake recrystallization, achieving authentic flaky texture, moisture retention, and traditional appearance in sugar-free national sweets.
Erythritol provides a clean, sucrose-like sweet curve without the lingering metallic aftertaste associated with intense sweeteners. When formulated into fruit sherbets, ice teas, and functional soft drinks, its negative heat of solution (-43 cal/g) imparts an enhanced sensory feeling of crisp refreshing coolness, ideal for the warm Caspian climate.
Industrial dairies across Azerbaijan utilize fine 100-mesh Erythritol in fermented dairy matrices. Because Erythritol cannot be metabolized by standard lactic acid starter cultures (such as Lactobacillus bulgaricus), it maintains stable sweetness levels throughout extended cold-chain storage without causing unwanted secondary fermentation or acidity changes.
Baku-based pharmaceutical co-packers utilize pharmaceutical-grade Erythritol as a non-cariogenic filler and binder for chewable vitamin tablets, diabetic syrups, and oral care products. Its non-hygroscopic nature (does not absorb moisture below 90% relative humidity) ensures long shelf-life and prevents tablet degradation.
Micronized Erythritol powder (< 50 microns) integrates into chocolate conching machines without causing grittiness. In fat-based systems, it yields viscosity, snap, and melt characteristics highly comparable to premium cocoa butter-sucrose solids, enabling compliant clean-label sugar-free chocolate production.
To match exact sucrose sweetness profiles (100% sweetness strength), our factory formulates co-crystallized or dry-blended mixtures of Bulk Erythritol with high-intensity steviol glycosides (Reb-A / Reb-M), Monk Fruit extract, or Sucralose, eliminating upfront R&D work for local manufacturers.
Procuring wholesale food raw materials through multi-tiered European or regional brokerage networks frequently introduces inflated landed costs, erratic batch availability, and fragmented quality documentation. Partnering directly with a premier Chinese Erythritol bulk manufacturing complex provides structural supply chain resilience for Azerbaijani operations.
By leveraging Chinese industrial fermentation scale and raw material integration (Shandong corn agricultural belt), enterprise buyers access tier-1 wholesale pricing structures impossible for localized distributors to match, protecting your gross product margins.
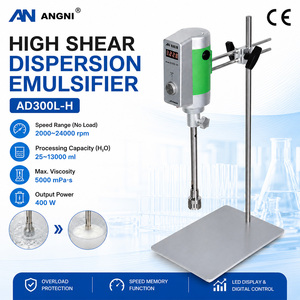
Streamline your procurement workflow. Combine bulk Erythritol orders in a single container with modified starches, pea protein isolates, dehydrated garlic, hydrocolloids, and precision processing machinery under one consolidated Commercial Invoice and Packing List.
We mitigate working capital strain by supporting flexible Minimum Order Quantities (MOQs) starting from single FCL (Full Container Loads) or consolidated LCL shipments, packaged in 25-kg multi-wall kraft paper bags, 500-kg super-sacks, or custom retail-ready pouches.
Every production batch is accompanied by comprehensive Certificates of Analysis (CoA), ISO22000, FSSC22000, Kosher, and Halal certifications fully compliant with the import health standards enforced by the Food Safety Agency of the Republic of Azerbaijan.
We manage direct multimodal logistics routes connecting Chinese manufacturing hubs via the Trans-Caspian International Transport Route (Middle Corridor) directly to Baku Port (Alat), minimizing transit lead times and eliminating ocean freight volatility.
Our dedicated R&D specialists assist your factory engineers with formulation adjustments, bench-top samples, solubility trials, and process optimization to ensure zero disruption during production line transitions.
Clear operational and regulatory answers to facilitate seamless cross-border raw material procurement.
Partner directly with China’s premier wholesale fermentation plant. Request factory-direct pricing, technical spec sheets, and complimentary sample kits delivered directly to your R&D laboratory in Azerbaijan.
Send an Inquiry