
Food Grade Indian Guar Gum Powder for International B2B Ingredient Procurement
Premium high-viscosity hydrocolloid tailored for sauce stabilization, bakery hydration, and frozen dessert freeze-thaw preservation.
Inquire NowFactory-direct wholesale food ingredients refined under stringent international quality protocols, delivered seamlessly to Greater Boston facilities.
Premium high-viscosity hydrocolloid tailored for sauce stabilization, bakery hydration, and frozen dessert freeze-thaw preservation.
Inquire Now
High-oleoresin raw ginger root engineered for industrial extractors, condiment manufacturers, and ready-to-drink beverage processors.
Inquire Now
Heat-stable micro-encapsulated aromatic vanilla powder formulation built for commercial baking mixes, dairy, and confectionery.
Inquire Now
Dehydrated citrus wheel slices optimized for botanical brewing, specialty tea blending, and craft cocktail infusion systems.
Inquire Now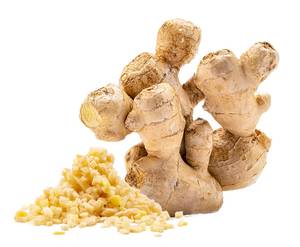
Pungent, washed fresh ginger roots shipped via temperature-controlled maritime containers for fresh purée and culinary applications.
Inquire Now
99.7% USP vegetable glycerine humectant ensuring moisture control, texture retention, and solvent purity in commercial food production.
Inquire Now
Non-GMO functional protein (70% dry basis) designed for water-binding, emulsification, and structure building in meat and plant foods.
Inquire Now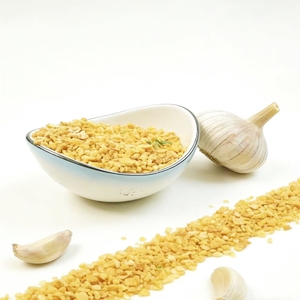
Crispy golden dehydrated garlic granules delivering aromatic crunch and savory depth for meal kits, soups, rubs, and snacks.
Inquire NowThe Greater Boston food manufacturing landscape—stretching from the maritime seafood processing complexes surrounding Boston Harbor and New Bedford to the artisan industrial bakeries of Chelsea, Everett, and Woburn—operates under rigorous supply chain expectations. As regional consumer demand shifts toward clean-label formulations, plant-based nutrition, and precise flavor profiles, food manufacturers face unprecedented pressure to secure consistent, high-purity raw materials directly from global manufacturing hubs.
As a premier China-based wholesale food ingredient manufacturer and exporter, our organizational model bridges transpacific manufacturing scale with localized New England delivery precision. Sourcing directly from certified Chinese agricultural and biochemical facilities eliminates intermediary markups while introducing rigorous quality verification prior to ocean transit. Navigating transpacific trade routes requires more than standard brokerage; it demands an integrated supply chain model encompassing factory-floor QA auditing, custom mesh sizing, anti-caking particle engineering, and strict compliance with the U.S. Food and Drug Administration (FDA) and Food Safety Modernization Act (FSMA) standards.
Recent infrastructure modernizations at Boston’s Conley Container Terminal (including deepened berths and direct intermodal connections) allow for direct ocean vessel calls from major Asian ports. By leveraging direct shipping lines to Boston, food processors eliminate the congestion and drayage delays traditionally experienced at West Coast ports or inland freight hubs in Chicago.
Our localized supply chain architecture pairs direct container shipments to Conley Terminal with regional buffer warehousing near the I-95/I-90 logistical corridors in Massachusetts and Pennsylvania, providing Boston food manufacturers with uninterrupted access to essential hydrocolloids, starches, dehydrated vegetables, and functional proteins.
How raw materials engineered at our direct manufacturing plants solve complex formulation challenges across New England’s core food clusters.
Greater Boston and New Bedford process over 40% of Atlantic seafood products. Our Food Grade Indian Guar Gum and specialized food starches serve as crucial viscosity builders in canned clam chowder bases and frozen seafood glazes, preventing syneresis and maintaining thermal stability during commercial retort processing.
From commercial cannoli filling plants to large-scale dough mixing facilities in Chelsea and Revere, maintaining soft crumb structure and moisture activity is critical. Our Refined 99.7% USP Glycerine acts as an optimal humectant, while heat-stable micro-encapsulated Vanilla Powder ensures flavor retention under high thermal stress.
Cambridge’s food tech innovation center leads in alternative protein development. Our high-solubility Soy Protein Concentrate (70%) delivers excellent gelation, oil retention, and neutral flavor profiles required for clean-label plant-based burgers, dairy alternatives, and high-protein sports nutrition drinks.
Boston food brand owners are rapidly adopting strict compliance with FSMA 204 Key Data Elements (KDEs). Sourcing raw materials from China requires absolute lot-level transparency from factory harvest to Boston receiving docks. Our supply chain delivers full digital traceability certificates, COAs (Certificates of Analysis), and heavy metal residue testing for every imported batch.
Traditional New England regional brokers add 15% to 30% in cost markups without providing manufacturing oversight. Greater Boston procurement directors are bypassing multi-tiered distribution by negotiating directly with primary Chinese export manufacturers while relying on regional warehousing for Just-in-Time (JIT) safety stock buffering.
Combining large-scale Chinese manufacturing infrastructure with stringent international quality assurance protocols.
Direct oversight of raw material cultivation, from non-GMO soy fields to dehydrated garlic harvests, eliminating third-party agent risk.
Every shipment undergoes HPLC analysis, microbiological testing, micro-particle sizing, and heavy metal screening in ISO 17025 accredited labs.
Consolidate multiple functional raw materials (hydrocolloids, seasonings, glycerine) into single container loads to maximize freight density.
Strategic local inventory holding near Boston allows fast 24-to-48-hour delivery, reducing working capital lockup for local buyers.
Technical, regulatory, and logistical answers tailored for food and beverage ingredient buyers in Massachusetts.
We utilize direct ocean shipping routes from ports in Shanghai, Qingdao, and Ningbo directly to Conley Container Terminal in Boston. Additionally, we maintain rolling buffer stock in regional New England warehouses (including Frazer, PA and Sayreville, NJ distribution nodes) to ensure immediate 24-48 hour replenishment for urgent plant requirements.
All products are supplied with comprehensive batch documentation, including ISO 22000, HACCP, FSSC 22000, Halal, Kosher, and USDA Organic certifications where applicable. Every shipment includes a detailed Certificate of Analysis (COA) confirming physical, chemical, and microbiological specs prior to customs clearance.
Yes. While we export FCL containers directly to high-volume processors, our order consolidation program allows small and medium-sized Boston food producers to combine smaller palletized quantities (LCL) of different raw materials—such as Soy Protein Concentrate, Guar Gum, and Dried Garlic—into a single consolidated delivery.
Our technical application specialists provide bench-to-scale guidance. If you are replacing synthetic emulsifiers or binders, we supply technical data sheets, sample batches of natural hydrocolloids or plant proteins, and advice on viscosity performance under variable processing temperatures.
We work with specialized licensed customs brokers in Boston to ensure precise HTS (Harmonized Tariff Schedule) classification. Through factory-direct pricing, optimized shipping tariffs, and consolidated freight logistics, we offset tariff costs to keep landed ingredient prices highly competitive.
Simply click our "Inquire Now" button anywhere on this page to initiate live technical support. Our transpacific sales team will verify your product specifications, send pre-shipment sample kits, and provide detailed landed cost estimates tailored to your delivery docks in Massachusetts.