In the competitive landscape of Victoria’s food processing industry—spanning Gippsland dairy plants, Geelong meat processors, and Greater Melbourne artisanal bakeries—achieving batch-to-batch structural stability, moisture control, and shelf-life extension demands rigorous chemical consistency. As a dedicated OEM/ODM Food Grade Phosphates Factory & Direct Supplier, we deliver technical-grade, FSANZ-compliant monophosphates, diphosphates, tripolyphosphates, and polyphosphates engineered specifically for local processing requirements.
Navigating international supply chains while maintaining strict compliance with Food Standards Australia New Zealand (FSANZ Standard 1.3.1) requires more than off-the-shelf chemical sourcing. It requires custom particle size distribution (mesh sizing), tailored rate of reaction (ROR) for leavening acids, specialized bulk density matching, and consolidated procurement workflows that eliminate single-item shipping overheads.
High-purity chemical salts refined for meat processing, dairy stabilization, beverage acidulation, and bakery leavening across Victoria.
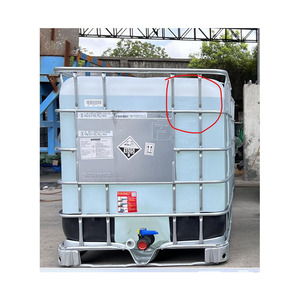
Essential inorganic acidulant used in cola beverage formulations, pH control, yeast brewing, and sugar refining processes.
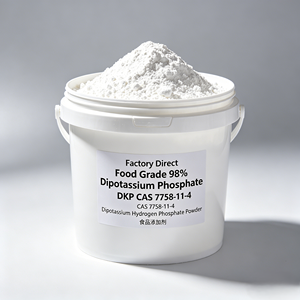
Premium low-sodium buffering salt for non-dairy creamers, UHT milk drinks, and mineral-fortified sports beverages.
Highly bioavailable calcium-phosphorus fortification agent for breakfast cereals, infant formulas, and bakery products.
Concentrated nutritional fortifier and tableting diluent providing maximum elemental calcium and phosphorus ratio.
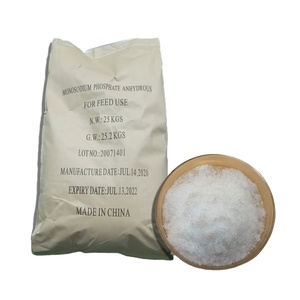
Versatile pH regulator, acidulant, and anti-caking buffer ideal for dry mix soup blends and beverage processing.
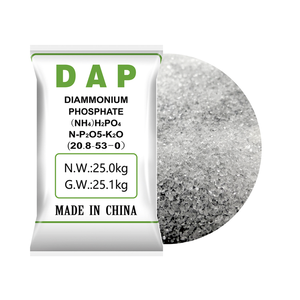
Essential yeast nutrient for wine fermentation in Yarra Valley wineries, craft breweries, and industrial baking processes.
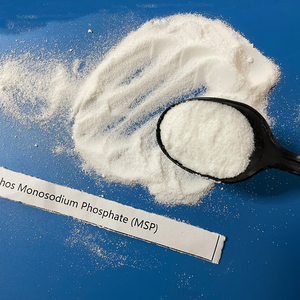
High-purity food-grade MSP ensuring rapid dissolution, precise acidity adjustment, and protein stabilization.
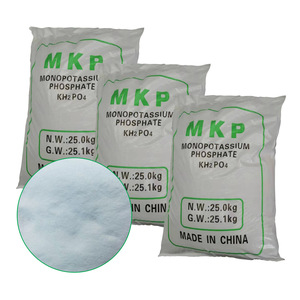
Premium sodium-free buffering agent and nutrient source tailored for electrolyte formulations and specialty food lines.
Food-grade phosphates perform distinct biochemical roles based on their chain length, ionic charge, and buffering capacity. The table below outlines chemical functions tailored to Victoria's primary food sub-sectors:
| Phosphate Compound | Primary Functionality | Target Food Sub-Sector | FSANZ Code / Regulatory Standard |
|---|---|---|---|
| Phosphoric Acid (75%, 85%) | Acidulant, pH Reducer, Beverage Clarifier | Carbonated Soft Drinks, Cider, Sugar Refining | Standard 1.3.1 - E338 |
| Dipotassium Phosphate (DKP) | Protein Stabilizer, Mineral Buffer, Anti-feathering | UHT Dairy, Plant-based Milks, Coffee Creamers | Standard 1.3.1 - E340(ii) |
| Dicalcium Phosphate (DCP) | Calcium/Phosphorus Fortification, Flow Agent | Infant Formulas, Nutritional Bars, Extruded Foods | Standard 1.3.1 - E341(ii) |
| Monosodium Phosphate (MSP) | pH Buffering, Emulsification, Color Retention | Processed Cheeses, Evaporated Milk, Dry Mixes | Standard 1.3.1 - E340(i) |
| Diammonium Phosphate (DAP) | Yeast Assimilable Nitrogen (YAN) Source | Wine Fermentation, Brewing Yeast Propagation | Processing Aid - Fermentation |
| Monopotassium Phosphate (MKP) | Sodium-Free Electrolyte Buffer, Moisture Agent | Low-Sodium Meat Products, Sports Nutrition | Standard 1.3.1 - E340(i) |
From Gippsland's automated dairy processing plants to Yarra Valley's boutique wineries, our OEM formulations solve specific regional production bottlenecks.
In ultra-high temperature (UHT) milk production and condensed dairy lines across Victoria, heat-induced protein denaturation can trigger gelation and phase separation. Utilizing customized blends of Dipotassium Phosphate (DKP) and Monosodium Phosphate (MSP) adjusts the ionic strength of milk proteins, preventing feathering in hot acidic environments like coffee and guaranteeing 12-month ambient shelf-life stability for export markets.
Industrial baking operations in Dandenong and Campbellfield require exact Rate of Reaction (ROR) control during automated leavening. Our custom-milled Dicalcium Phosphate (DCP) and sodium acid pyrophosphate blends provide controlled carbon dioxide release during proofing versus baking, resulting in uniform crumb texture, optimal loaf volume, and enhanced moisture retention in packaged baked goods.
Victoria’s premium beef, lamb, and seafood processors face strict yield loss challenges during freezing, thawing, and cooking cycles. OEM polyphosphate and orthophosphate formulations elevate the pH of muscle tissue away from its isoelectric point. This expands protein structures, increases water-binding capacity, prevents thaw-drip loss, and preserves cooked meat succulence without imparting bitter chemical aftertastes.
Optimal yeast metabolism during grape juice fermentation requires precise Yeast Assimilable Nitrogen (YAN) levels. Our food-grade Diammonium Phosphate (DAP) serves as a clean, highly soluble nitrogen supplement for Victorian winemakers and craft distillers, preventing sluggish or stuck fermentations while suppressing hydrogen sulfide off-flavors in cold-fermented white and red wines.
With Melbourne emerging as a regional hub for health and fitness supplement manufacturing, our micronized Mono Potassium Phosphate (MKP) and Dicalcium Phosphate powders deliver clean elemental potassium, calcium, and phosphorus. These compounds maintain high solubility in powder blends and instant dry mixes, supporting clean-label positioning and rapid body absorption.
Australian consumer health guidelines and front-of-pack Health Star Ratings are driving Melbourne food technologists to reduce sodium levels in processed meats, ready-to-eat meals, and dairy products. We specialize in ODM sodium-to-potassium phosphate substitution, replacing conventional sodium tripolyphosphate with high-purity Dipotassium Phosphate (DKP) and Monopotassium Phosphate (MKP) to maintain essential texturizing benefits while drastically slashing overall sodium content.
Importing raw food chemicals into Australia requires absolute compliance with Food Standards Australia New Zealand protocols. Every batch produced in our OEM manufacturing facility undergoes stringent heavy metal screening (monitoring lead, arsenic, cadmium, and fluoride limits). Fully documented Certificates of Analysis (CoA), non-GMO declarations, and Kosher/Halal accreditations are automatically attached to every shipment landing at the Port of Melbourne.
Global shipping volatility has rendered traditional overseas procurement risky for continuous production schedules. Victorian food producers cannot afford plant downtime due to stranded ingredients. By partnering with us, clients leverage localized warehouse buffer programs across Victoria, ensuring guaranteed safety stock, consolidated shipment options, and rapid dispatch directly to regional processing facilities.
Industrial formulators increasingly demand ingredients optimized for high-speed automated dosing equipment. Our factory provides custom micronization, agglomeration, and anti-caking surface treatments. This yields dust-free, highly flowable powders that dissolve instantly in cold brine tanks or liquid milk streams without clogging automated pump valves.
Combining direct-factory chemical synthesis with enterprise-grade distribution capabilities to streamline your raw material supply chain.
Eliminate vendor clutter and accounts payable fatigue. Through our comprehensive catalog of 3,000+ food ingredients—ranging from starches and hydrocolloids to food phosphates and preservatives—you can source your complete formulation requirement under a single consolidated purchase order.
Buying directly from overseas primary chemical synthesis plants usually requires full container load (FCL) commitments. We support Melbourne's growing artisan processors and regional co-packers by offering flexible, lower minimum order quantities (MOQs), allowing you to optimize working capital and minimize warehouse footprint.
Our technical food technologists assist R&D teams with ingredient substitution, clean-label reformulations, and trial batching. We provide full laboratory samples, detailed specification sheets, and application troubleshooting from bench test stage all the way to commercial scale-up.
Clear, expert answers regarding regulatory standards, shipping options, custom formulations, and batch quality control.
Connect with our technical sales engineering team to discuss your target chemical specifications, FSANZ regulatory needs, or custom OEM phosphate blending requirements in the Melbourne market.
