Toll-free: 1 (800) 441-1017 HQ: 9 Lee Blvd, Frazer, PA 19355
3,000+ ingredients · One purchase order · On time, in full

Palm Oil Bulk Manufacturers & Exporters Serving the United States Market

Industrial-grade palm oil, olein, stearin, and specialized fractions engineered for food manufacturing, foodservice supply chains, and oleochemical processing across North America.

3,000+
Ingredients Managed
100%
FSVP & RSPO Compliant
< 0.1%
Free Fatty Acid (FFA) Standard
24/7
U.S. East Coast Warehouse Access

Essential Food Ingredients & Bulk Lipids Portfolio

Discover our high-purity functional ingredients, texturizers, and flavor systems designed for U.S. food processing, industrial baking, and beverage production lines.
Artificial Beer Oil Soluble Flavor Food Grade
Artificial Beer Oil Soluble Flavor Food Grade For Braised Products Sauce Hot Pot Base Marinade Compound Seasoning
Get a Quote
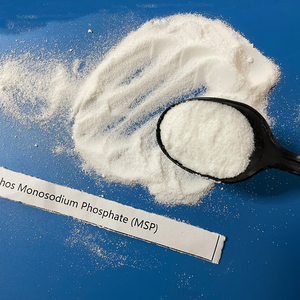
98% Purity Monosodium Phosphate MSP
Made in China Factory Direct Sale Hot-sale Products 98% Purity Monosodium Phosphate MSP for Food
Get a Quote
Halal Savory Flavor Meat Processing Ingredient
Halal Savory Flavor Meat Processing Ingredient BBQ Aroma Essence Authentic Roast Meat Flavor for Sausages Instant Noodles Snacks
Get a Quote
Dehydrated Garlic Powder
Liansheng High Quality Baked Dried Ad Dehydrated Garlic Powder Good Price Single Spice Powder
Get a Quote
Peanut Oligopeptide Powder
Bulk Supply Food Grade Natural Nutritional Enhancement Peanut Extract 98% Peanut Oligopeptide Powder
Get a Quote
Bulk Spirulina Powder Wholesale
Green Source Bulk Spirulina Powder Wholesale High-Quality Nutraceutical-Grade Spirulina Supplier
Get a Quote
Petop Cat Food Ingredients High Protein Taurine
Petop Cat Food Ingredients Premium Quality Natural Sources High Protein Taurine Cat Food Ingredients for Complete Nutrition
Get a Quote
Food Grade Chicken Flavor Essence Liquid
Food Grade Low Cost Chicken Flavor Essence Liquid Concentrated Fragrance for Snack Instant Noodles and Savory Food Flavor
Get a Quote

Industrial Palm Oil Supply Chain: Technical White Paper & U.S. Market Dynamics

As North American food manufacturers shift away from partially hydrogenated oils (PHOs) to meet FDA mandates and consumer demand for clean-label, zero-trans-fat products, refined, bleached, and deodorized (RBD) palm oil has emerged as the premier structural lipid across the United States. Serving as an essential functional fat, palm oil provides tailored solid fat content (SFC) profiles, exceptional oxidative stability, and neutral organoleptic performance without requiring chemical hydrogenation.

However, securing reliable bulk shipments of crude palm oil (CPO), palm olein, and palm stearin across global supply chains requires deep expertise in ocean logistics, international customs compliance, and rigorous quality control. U.S. food processors face volatile commodity markets, strict FDA Foreign Supplier Verification Program (FSVP) enforcement, and escalating standards regarding sustainable sourcing (RSPO Mass Balance and Segregated supply chains). As a premier bulk manufacturer, global exporter, and U.S. distributor partner, we bridge Southeast Asian production facilities directly with American manufacturing facilities through optimized freight networks and localized warehousing hubs.

Localized U.S. Industrial Application Scenarios

Palm oil fractions are precisely calibrated for distinct thermal, structural, and shelf-life requirements across American food manufacturing sectors.

1. Commercial Bakery & Industrial Shortenings

In wholesale baking facilities throughout the U.S. Midwest and Mid-Atlantic, customized RBD palm oil blends replace traditional shortening. Palm oil’s unique beta-prime (β′) crystal habit creates smooth fat networks essential for pie crust lamination, biscuit fluffiness, and cake aeration. High-stearin fractions deliver structural plasticity, preventing oil bleeding during automated dough handling.

2. High-Stability Deep Frying (Snack Food Industry)

Industrial potato chip, tortilla chip, and donut producers rely on RBD Palm Olein (Iodine Value IV 56–60). With a high smoke point (> 450°F / 232°C) and low linolenic acid content, palm olein resists thermal polymerization, oxidative breakdown, and free fatty acid (FFA) accumulation, drastically extending fry-life compared to liquid soybean or canola oils.

3. Confectionery & Cocoa Butter Substitutes (CBS)

Precision-fractionated palm mid-fractions (PMF) function as physical Cocoa Butter Equivalents (CBE). In compound chocolate coatings, confectionery fillings, and melt-in-the-mouth center creams, PMF yields sharp melting profiles right at body temperature (37°C), delivering pristine gloss retention, snap, and heat resistance during summer distribution across North America.

4. Oil-Soluble Carrier Systems & Flavor Matrices

Specialty oil-soluble food flavors—such as savory meat aromas, beer flavor compounds, and roast essences—require high-purity, ultra-bland liquid palm carriers. Ultra-refined palm olein prevents flavor oxidation, ensures homogeneous dispersion in hot pot bases, marinades, and seasoning slurries, and preserves volatile top-notes during thermal processing.

5. Pet Nutrition & Oleochemical Formulations

In premium pet foods (cat food kibble top-coatings, complete nutritional pastes), refined palm fats supply dense energy, essential fatty acids, and carrier stability for fat-soluble vitamins (A, D, E) and taurine additives. Additionally, U.S. industrial oleochemical producers utilize bulk palm fatty acid distillate (PFAD) for eco-friendly surfactants, soaps, and bio-lubricants.

U.S. Market Trends & Regulatory Compliance Integration

RSPO & Deforestation-Free Mandates

U.S. consumers and major retail chains demand 100% verifiable sustainability. Supply chain transparency is paramount. We offer fully certified Roundtable on Sustainable Palm Oil (RSPO) supply chains, including Mass Balance (MB) and Identity Preserved / Segregated (SG) options. Our plantation partners adhere to No Deforestation, No Peat, No Exploitation (NDPE) policies, ensuring total compliance with upcoming U.S. FOREST Act legislation.

FDA Foreign Supplier Verification (FSVP)

Navigating U.S. Customs and FDA regulations requires meticulous documentation. Every ocean flexitank and bulk vessel shipment entering ports like New York/New Jersey, Philadelphia, or Houston undergoes exhaustive testing for heavy metals, pesticide residues, 3-MCPD, and glycidyl esters (GE). We provide complete FSVP dossier verification, Certificates of Analysis (CoA), Kosher, and Halal documentation for seamless entry.

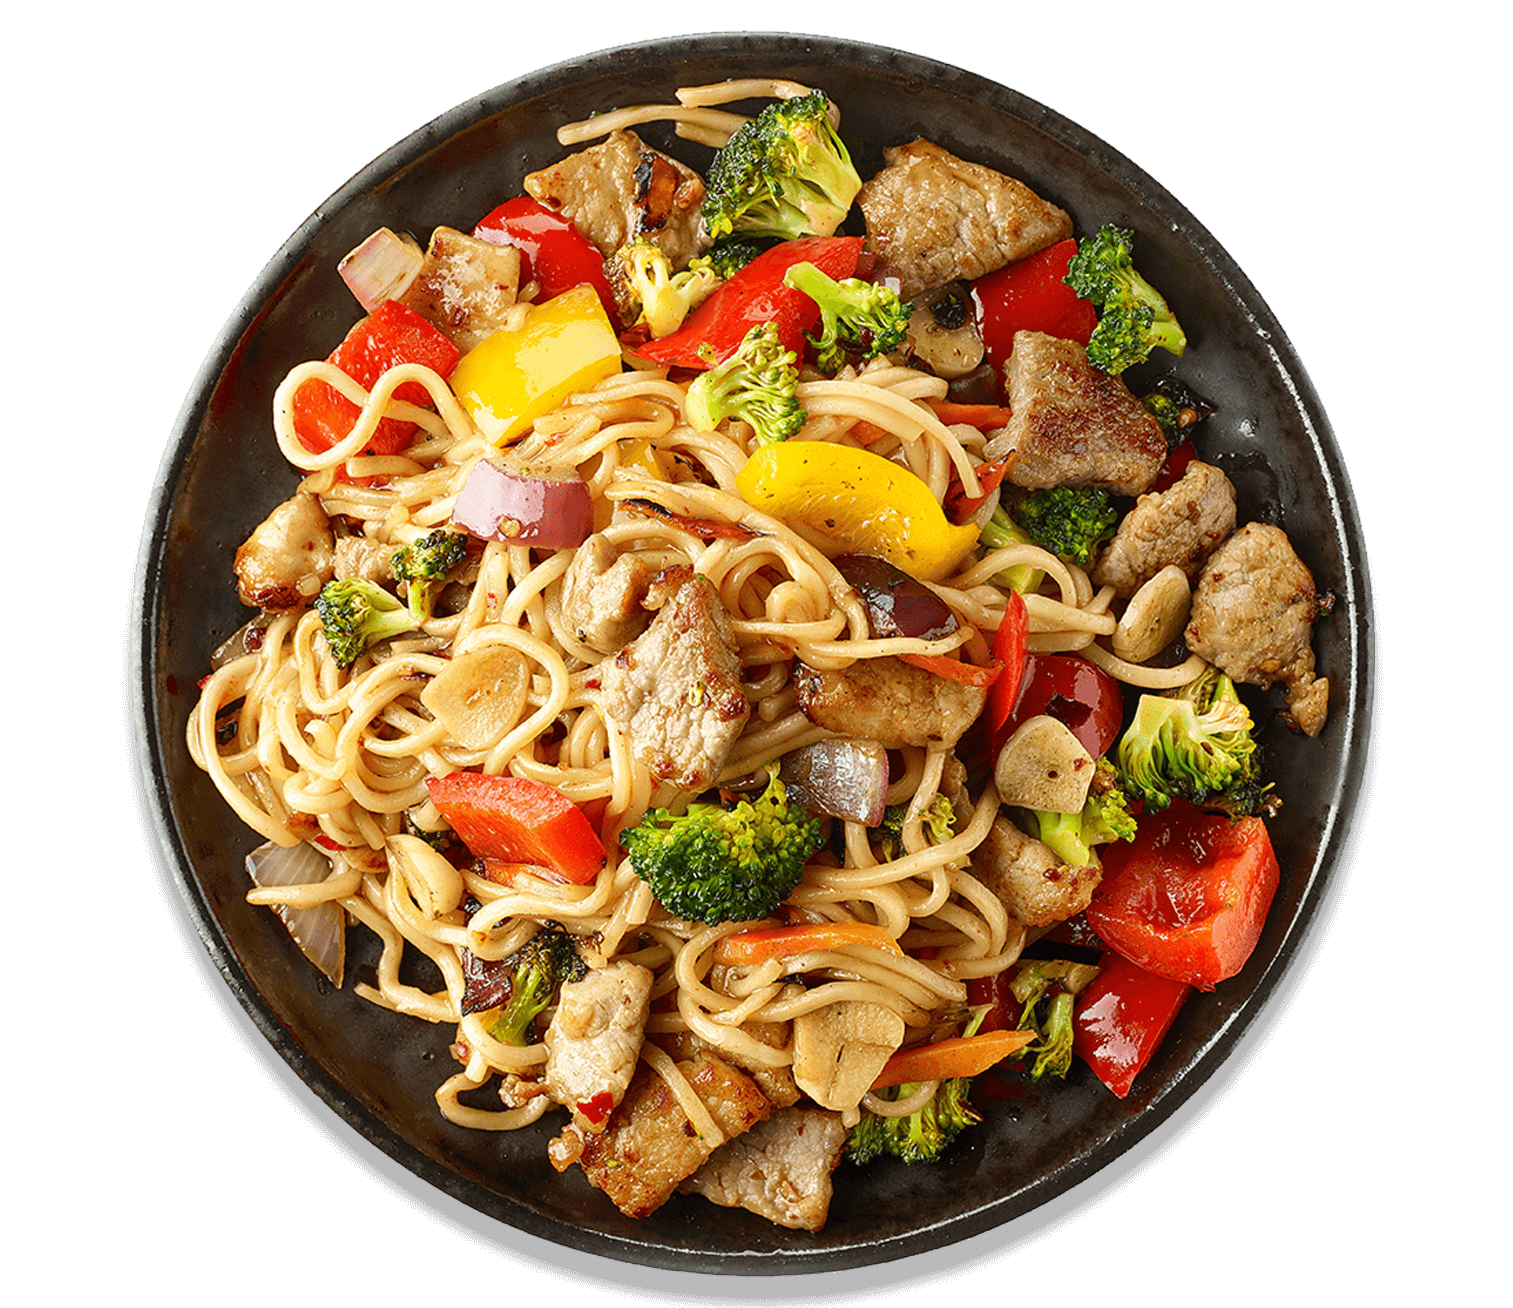
Industrial food manufacturing utilizing palm oil fats

Modern U.S. food formulation strategies focus heavily on clean labeling and non-GMO consistency. Because palm oil is natively non-GMO and naturally semi-solid at ambient temperature, formulators eliminate the need for chemical interesterification or hydrogenated trans-fats. This allows U.S. brands to claim "0g Trans Fat Per Serving" on packaging while keeping production line equipment running without costly reconfiguration.

Enterprise Supply Chain Solutions: The Essex Advantage

Partnering with Essex Food Ingredients simplifies complex ingredient procurement through order consolidation, regional inventory, and technical R&D support.

Single PO Consolidation

Simplify procurement by purchasing bulk palm lipids alongside 3,000+ functional ingredients—including starches, hydrocolloids, dehydrated garlic powder, monosodium phosphate (MSP), and savory flavor bases—on a single purchase order.

Flexible MOQ & Rapid Delivery

Avoid working capital lockup. Leveraging our strategic distribution hubs in Frazer, PA, and Sayreville, NJ, we stock bulk flexitanks, IBC totes, and 55-gallon drums, providing short lead times and lower Minimum Order Quantities (MOQs) than direct overseas mills.

R&D & Formulation Support

Our food technologists collaborate with your bench R&D team to optimize Solid Fat Content (SFC) curves, resolve oil-bleeding in baked goods, match precise melting profiles, and fine-tune oil-soluble flavor dispersion.
Representing Global Ingredient Leaders & Supply Chain Partners

Cargill
Stratas Foods
Glanbia
Tate & Lyle
Ingredion
Innophos

Frequently Asked Questions for U.S. Bulk Buyers & Procurement Teams

Get detailed technical and logistical answers regarding bulk palm oil importation, storage, quality parameters, and regulatory compliance.

What bulk packaging formats are available for delivery within the United States?
We supply industrial palm oil across multiple flexible volume formats tailored to your plant setup:
  • Flexitanks (24,000 Liters / ~44,000 lbs): Ideal for ocean transport directly to plant receiving bays with liquid pumping stations.
  • ISO Tank Containers: Reusable stainless-steel tanks for high-volume automated manufacturing lines.
  • IBC Totes (2,000 lb / 275 Gal): Disposable or returnable liquid totes with bottom-discharge valves.
  • 55-Gallon Steel Drums (420 lbs net): Palletized for mid-sized bakeries and flavor processing houses.
How do you prevent palm oil crystallization and setup during cold winter transit in North America?
RBD Palm Oil and Palm Stearin have natural melting points between 95°F and 126°F (35°C–52°C). During winter shipping across Northern U.S. transit routes, liquid fat will naturally solidify. Our bulk flexitanks come equipped with low-pressure steam or hot-water heating pads beneath the liner. Plants can connect hot water lines 12–24 hours prior to discharge to safely melt the oil back to liquid state without causing thermal scorch or elevated peroxide values.
What is the difference between Iodine Value (IV) 56 Olein and IV 60 Superolein?
Iodine Value (IV) measures the degree of unsaturation in fatty acid chains:
  • Standard RBD Palm Olein (IV 56): Has a cloud point of approximately 10°C (50°F). It is widely used for industrial deep frying and baking shortenings.
  • RBD Palm Superolein (IV 60–64): Undergoes double fractionation, remaining liquid at cooler temperatures (cloud point < 6°C / 42°F). Superolein is preferred as a clear retail salad oil blend, cooking oil spray, and as a low-viscosity carrier for oil-soluble food flavors and colorants.
How does your supply chain meet FDA Food Safety Modernization Act (FSMA) requirements?
As a registered domestic supplier, Essex Food Ingredients operates under strict FSMA Hazard Analysis Risk-Based Preventive Controls (HARPC). All overseas refineries are vetted under our Foreign Supplier Verification Program (FSVP). Every shipment is accompanied by a lot-specific Certificate of Analysis (CoA) testing for Free Fatty Acids (≤0.1%), Peroxide Value (≤1.0 meq/kg), Moisture & Impurities (≤0.05%), and heavy metals.
Can we request RSPO Segregated (SG) certified palm oil for clean-label U.S. consumer products?
Yes. We offer fully traceable RSPO Segregated (SG) palm products, keeping sustainable oil 100% physically separated from non-certified oil from the origin mill all the way to your U.S. factory dock. RSPO Mass Balance (MB) options are also available for cost-sensitive sustainability initiatives.
What is the typical shelf life of RBD Palm Oil under standard U.S. warehouse storage?
RBD Palm Oil features outstanding natural oxidative stability due to its balanced fatty acid profile (approx. 50% saturated, 40% monounsaturated, 10% polyunsaturated) and naturally occurring tocotrienols (Vitamin E). When stored in sealed containers at 65°F–75°F away from direct sunlight, bulk palm oil maintains a prime shelf life of 12 to 24 months without requiring artificial antioxidants like TBHQ or BHA.

Optimize Your Bulk Palm Lipid & Ingredient Supply Chain Today

Contact our technical sales team to request product specification sheets, CoA documentation, RSPO chain-of-custody verification, or bench test samples for your manufacturing facility.